


 The Fearless Connector: Why I Chose the Hard Road
 The Clean Truth: The Clean Truth About No-Clean Flux
 Global Sourcing Spotlight: Beyond China Plus One—Building a Truly Global Supply Network
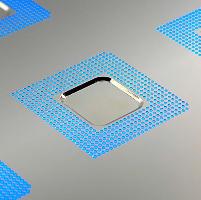
I recently met with Eric Weissmann, president and CEO of Photo Stencil. In this interview, Weissmann shares some important points about the venerable stencil, the latest in stencil innovation, and the impact stencils, blades, and cleanliness can have on your product quality.
Barry Matties: Why don’t you just start by telling me a little bit about Photo Stencil?
Eric Weissmann: Sure, I’d be pleased to. Photo Stencil has been around since the early ‘70s making stencils, screens, and squeegee blades primarily for the SMT industry. Historically, there has been a continuum of products and demand for products for printing materials, from back in the old days with chemically etched stencils up to the modern, multidimensional 3D electroform type stencils. What we’re seeing now is that there’s been a bifurcation in the market for these stencils as well as simple ones that are served by laser-cut stencils. It’s a piece of stainless steel that a laser cuts apertures through, which solder paste can then print through. That’s on the one hand, and then there are the much more advanced applications with smaller features, products going into harsher environments, advanced packaging, and electrical interconnects on the micron scale. That is where we see our future.
For the last 18 months or so we’ve been making a lot of investments in our capability and our facilities to be prepared for where we see the market going.
Matties: What do you think of the new jet style applications?
Weissmann: Dispensing versus printing is the broader question, and of course dispensing is a “dot at a time” kind of thing. It’s a lot slower. We have the same kind of thing internally, the one-at-a-time versus a parallel process. When we make an electroform stencil, we do everything at once; a laser-cut stencil is cut one aperture at a time. If you have a wafer with a million things that need to be printed, that’s going to be hours and hours instead of seconds. Speed is the fundamental difference. Other differences of course are accuracy, dimensionality, and flexibility in a stencil. Like dispensing, both technologies can print different kinds of materials. It can print flux and it can print paste.
The thing I see the most is just what everyone sees in terms of ever-smaller components and ever-tighter density. Right now we’re looking at 01005 passives being quite routine, and our customers are talking about smaller passives in the relatively near future. Micro QFNs and other components are posing real challenges for people in assembly. What we’re seeing are some of the companies making simpler products are using simpler stencils, but there’s real value for OEMs—where the ultimate product goes into a harsh environment, like an automobile or an aircraft, or into something going into the human body like a medical device—to use a better stencil to get better paste transfer, but also a better quality mechanical electrical connection there at the joint.
Matties: You’re talking about higher quality stencils. When a customer is looking at millimeter application, what should the considerations be?
Weissmann: The customer should be looking at the area ratio of the stencil, the ratio of the flat side of the pad that they want to print to the walls of the stencil, and how thick it has to be. The smaller that ratio is, the harder it is to transfer those things. You want to have a stencil with a smoother material, and that’s a pure nickel stencil rather than a steel stencil. You also would like to have a stencil that has been electroformed, because you end up with smoother walls on the inside of the aperture, so it’s easier for the material being printed to get through.
One of the things that we’ve added this year is a laser imaging system in place of our traditional photo process, and that produces even more accurate and even smoother walls for more challenging printing applications.
Editor's Note: This article originally appeared in the August 2015 issue of SMT Magazine.


